

Water is at the core of almost every industrial process, and its quality directly affects product quality, equipment life and operating cost. For industries that cannot compromise on purity, reverse osmosis (RO) is the technology of choice. The RO membrane is the central separation element in a modern treatment system. It removes dissolved salts, heavy metals, bacteria, viruses and many chemical contaminants with a high degree of reliability, and it is used everywhere from pharmaceutical manufacturing and food processing to seawater desalination and municipal supply.
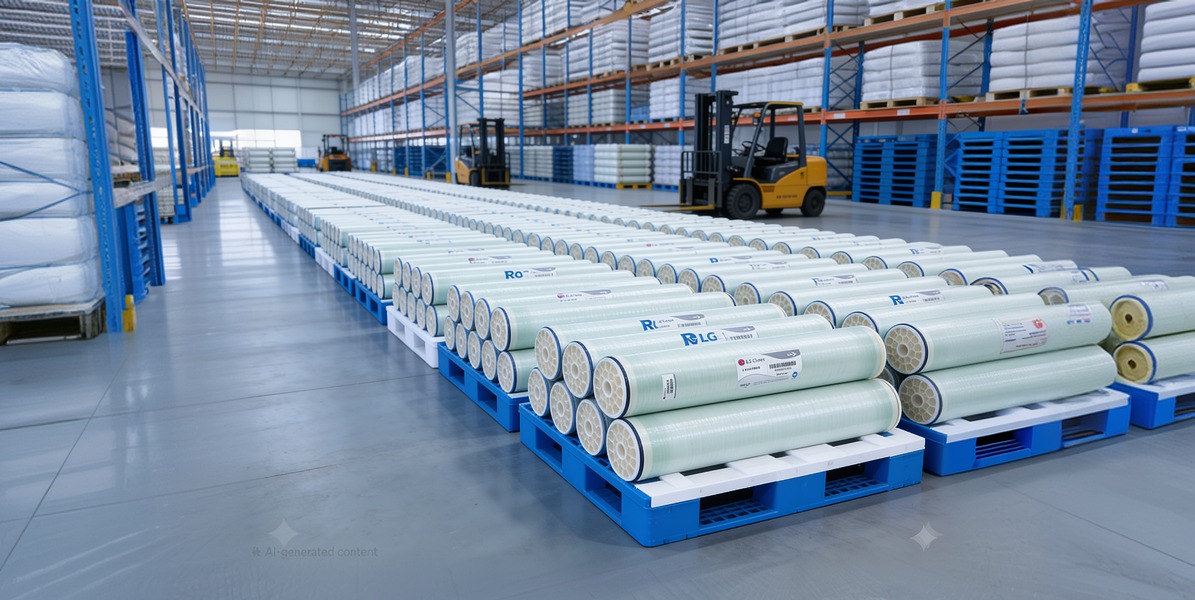
Selecting the right membrane, maintaining it correctly and understanding what affects its performance are not always straightforward decisions. This guide covers all of it in one place. Whether you are evaluating membranes for a new system, troubleshooting a loss of output or planning a replacement, you will find practical information here to support the decision.
Table of Contents
- What Is a RO Membrane?
- How Does a RO Membrane Work?
- Key Benefits of RO Membranes
- Main Components of a RO System
- Types of RO Membranes
- Common Membrane Materials
- Standard RO Membrane Sizes
- Industrial Applications of RO Membranes
- Factors Affecting RO Membrane Performance
- Common Causes of Membrane Fouling
- Signs Your RO Membrane Needs Replacement
- RO Membrane Cleaning and Maintenance
- How to Extend RO Membrane Life
- Popular RO Membrane Brands
- How to Choose the Right RO Membrane
- Why Choose Aqua Flair for RO Membranes in the UAE and GCC?
- Frequently Asked Questions
- Conclusion
What Is a RO Membrane?
An RO membrane is a semi-permeable barrier used in reverse osmosis systems to separate dissolved salts, contaminants, bacteria and other impurities from water. Under applied pressure, water molecules pass through the membrane while most dissolved solids and contaminants are rejected and discharged as concentrate. The result is a continuous supply of high-purity water for demanding industrial and commercial use.
RO membranes are used across a wide range of sectors, including:
- Industrial water treatment plants
- Commercial water purification systems
- Seawater desalination plants
- Food and beverage production facilities
- Pharmaceutical manufacturing
- Hotels, hospitals and large commercial buildings
- Manufacturing and processing industries
Related article: What Is an RO Membrane and How Does It Work?
How Does a RO Membrane Work?
Reverse osmosis applies pressure to the feed water (the raw incoming water) and forces it through a semi-permeable membrane. The membrane lets water molecules through while blocking dissolved salts, contaminants and microorganisms. The process produces two streams:
Permeate water. The purified water that passes through the membrane. This is the treated output used in your process or application.
Concentrate water (reject stream). The water that does not pass through. It carries the rejected salts and contaminants out of the system.
A properly specified and maintained RO membrane can remove:
- Dissolved salts and minerals
- Heavy metals, including lead, arsenic, mercury and chromium
- Organic chemical compounds
- Bacteria and microorganisms
- Viruses
- Suspended particles and sediment
Most industrial elements are spiral wound: flat membrane sheets separated by feed spacers and wrapped around a central permeate tube. Several elements sit in series inside a pressure vessel, and vessels are arranged in stages to reach the recovery the application needs. For a plain-language overview of the technology, read Reverse Osmosis (RO): The Purest Water Solution.
Key Benefits of RO Membranes
Industrial-grade RO membranes offer practical advantages that make them the preferred purification technology across many sectors.
High salt rejection. Modern thin-film composite (TFC) membranes achieve salt rejection from about 96% to over 99.7%, which makes them effective even on heavily contaminated feed water.
Consistent water quality. RO delivers stable permeate quality over long periods, provided operating conditions are respected and maintenance is managed.
Lower long-term operating cost. The right membrane, combined with effective pretreatment and scheduled maintenance, reduces chemical use, energy use and unplanned downtime.
Broad application range. From brackish water treatment and seawater desalination to pharmaceutical-grade water, RO adapts to a wide variety of industrial requirements.
Reduced environmental impact. RO reduces the need for chemical-intensive treatment and can be designed for high water recovery, which limits wastewater discharge.
Main Components of a RO System
A RO membrane operates as part of a complete system. Each component has a defined job in keeping performance consistent and protecting the membrane from early damage. For the wider picture of how the stages fit together, see How Water Treatment Systems Work.
Pretreatment filters
Pretreatment removes sediment, chlorine and other substances that could foul or chemically damage the membrane. It is one of the biggest factors in membrane longevity and is often underinvested during design. A typical train includes:
- Bag filters and high-flow filters for coarse and high-volume particle removal.
- FRP vessels holding filtration media such as sand and activated carbon for suspended solids, organics and chlorine. See Why FRP Pressure Vessels Are the Future of Water Filtration for why they suit RO duty.
- Clack valves to automate backwash and regeneration, explained in Clack Valves: The Smart Control Solution.
- Dosing pumps and dosing tanks for antiscalant, bisulphite and pH control.
- Cartridge filters, including pleated filter cartridges, as the final 5-micron guard before the high-pressure pump.
- Housings in stainless steel or uPVC. Filter Housing: The Foundation of Reliable Water Filtration helps you choose between them.
High-pressure pump
Generates the pressure that forces water through the membrane. Pump selection depends on membrane type, feed salinity and required flow.
RO membrane
The core separation element that removes dissolved contaminants from the feed stream.
Pressure vessel
A cylindrical housing that holds one or more membrane elements under operating pressure. RO pressure vessels must be rated for the system’s maximum operating pressure and sized for the element diameter.
Flow meters and instruments
A flow meter on the feed, permeate and concentrate lines shows changes that are often the first sign of fouling. Water quality meters track conductivity, TDS and pH.
Post-treatment equipment
Adjusts permeate quality after the membrane, for example remineralising water for drinking or fine-tuning pH for process needs.
Complete lines can also be supplied as a packaged RO system.
Types of RO Membranes
Membrane selection starts with the feed water source and its salinity. The two main categories are brackish water membranes and seawater membranes.
Brackish water membranes (BW)
Designed for feed water with low to moderate salinity, typically below about 10,000 mg/L TDS. They are the standard choice for:
- Municipal tap water and groundwater
- Well water and borehole supplies
- Industrial process water
BW membranes operate at lower pressure, which cuts energy use and makes them the most cost-effective option for most commercial and industrial applications.
Seawater membranes (SW)
Engineered for high-salinity feed, such as ocean water where TDS commonly exceeds 35,000 mg/L. Primary applications include:
- Coastal and offshore desalination plants
- High-salinity industrial water treatment systems
SW membranes need much higher operating pressure but deliver the highest salt rejection, above 99.7% in many specifications.
BW vs SW RO membrane comparison
| Feature | BW membranes | SW membranes |
|---|---|---|
| Feed water | Brackish, municipal, groundwater | Seawater, high-salinity water |
| Operating pressure | Lower (about 5 to 20 bar) | Higher (about 55 to 70 bar) |
| Salt rejection | High (about 96 to 99%) | Very high (about 99.3 to 99.8%) |
| Typical application | Industrial and commercial systems | Desalination plants |
| Energy requirement | Lower | Higher |
Related article: BW vs SW RO Membranes: What Is the Difference?
Common Membrane Materials
The membrane material determines salt rejection, chemical resistance and service life. Two materials account for most industrial production.
Thin-film composite (TFC) membranes
TFC is the industry standard for modern industrial and commercial water treatment. It is built in layers: a polyester support, a microporous polysulfone layer and an ultra-thin polyamide barrier, each engineered for a specific role. Key characteristics:
- Salt rejection: about 96 to 99.7% depending on specification
- Chemical compatibility: broad resistance to industrial cleaning chemicals
- Service life: strong long-term durability under stable conditions
- Permeate flow: higher output per unit area than CA membranes
Critical limitation. TFC membranes are sensitive to free chlorine. Even brief exposure can cause irreversible damage to the polyamide layer. Feed water must be fully dechlorinated, using activated carbon filtration or sodium metabisulphite dosing, before it reaches a TFC element.
Cellulose acetate (CA) membranes
An earlier-generation technology that remains in limited use. Its main advantage is chlorine tolerance: it can withstand small concentrations of free chlorine without degrading. Compared with TFC it has real limitations:
- Lower salt rejection
- Shorter operating life
- Susceptibility to biological degradation at certain pH levels
For most modern industrial RO systems TFC is the preferred choice. CA may be considered only where chlorine removal in pretreatment is not feasible.
Standard RO Membrane Sizes
Industrial RO membranes are made in standard dimensions so they fit different systems and manufacturers.
4040 membranes (4 in × 40 in). Used in smaller commercial systems such as restaurants, hotels, light industrial plants and point-of-use units. They have a compact footprint and suit lower-flow applications.
8040 membranes (8 in × 40 in). The standard for large-scale industrial RO. They deliver much higher permeate flow and are used in manufacturing, desalination, hospitals and municipal treatment.
Specialty sizes. Some applications need configurations outside the standard dimensions. These are specified at the design stage.
Size selection depends on required permeate flow, feed quality, system pressure rating and available space. The element diameter also decides the vessel you need, so plan both together.
Industrial Applications of RO Membranes
RO serves critical functions across many industries. In each case the shared requirement is consistently high-quality water that standard filtration cannot reliably deliver.
Food and beverage. RO produces process and ingredient water that meets strict purity and regulatory standards, from beverage and dairy production to juice concentration and packaged water.
Pharmaceutical. RO is the core of purified water (PW) production and a key step toward water for injection (WFI) systems that must meet standards such as USP, EP and WHO guidance. Consistency of water quality is non-negotiable in this sector.
Hotels and hospitality. Hotels, resorts and large commercial buildings use RO for drinking water, food preparation, laundry and HVAC, which improves guest experience and reduces equipment maintenance.
Manufacturing plants. RO treats boiler feed, cooling tower make-up and general process water across automotive, electronics, textile and chemical industries. Lower dissolved solids extend equipment life and cut chemical treatment cost.
Municipal water treatment. Utilities use RO to supply safe drinking water where groundwater salinity or contamination exceeds acceptable limits.
Seawater desalination. One of the most important RO applications globally. In water-scarce regions including the UAE and GCC, seawater RO is a primary source of potable water for communities and industry.
Factors Affecting RO Membrane Performance
A high-quality membrane will underperform if operating conditions fall outside its design envelope. These factors have the most direct effect on efficiency and service life.
Feed water quality. Poor feed quality is the leading cause of premature fouling. High suspended solids, organics, hardness or biological activity accelerate fouling and cut output. A thorough feed water analysis before design is essential.
Operating pressure. Each membrane type has an optimal pressure range. Operating below it reduces permeate output and efficiency. Operating far above the rated pressure can damage the membrane over time.
Water temperature. Permeability rises with temperature: warm feed passes through more easily, cold feed needs more pressure. Most specifications are rated at 25 °C (77 °F). In Gulf conditions, warm feed raises output but also speeds up biological growth.
Recovery rate. Recovery is the percentage of feed converted to permeate. Setting it too high concentrates dissolved solids and raises the risk of scaling. Recovery targets must match the feed water chemistry.
Pretreatment efficiency. The most influential factor in protecting a membrane. Well-pretreated water reduces fouling, extends cleaning intervals and increases membrane life.
Common Causes of Membrane Fouling
Fouling is the gradual build-up of material on or within the membrane. It is one of the most common operating problems in industrial RO and the main cause of declining performance. Identifying the type of fouling is essential for choosing the right cleaning method and preventing a repeat.
Scaling. Mineral salts, most commonly calcium carbonate, calcium sulphate, barium sulphate and silica, precipitate and form deposits. Scaling is most likely when recovery is too high or antiscalant dosing is insufficient for the feed chemistry.
Biological fouling (biofouling). Bacteria and other microorganisms colonise the surface and form a biofilm. It is a particular problem with inconsistent disinfection, warm temperatures or weak pretreatment. Once established, biofilm is hard to remove fully and tends to return.
Organic fouling. Natural organic matter, humic acids and oils adsorb onto the surface, blocking pores and reducing flux.
Colloidal fouling. Fine particles such as iron hydroxide, silica and clay deposit on the surface, raising differential pressure and cutting output.
Most fouling is preventable with sound pretreatment design, the right antiscalant and dose, and a consistent maintenance programme.
Related article: Common Causes of RO Membrane Fouling and How to Prevent Them
Signs Your RO Membrane Needs Replacement
RO membranes degrade gradually rather than failing suddenly. Decline is usually visible in routine monitoring well before end of life. These signs suggest replacement may be needed:
- Declining permeate flow: a sustained drop in output at the same pressure points to fouling or degradation that cleaning cannot fully reverse.
- Rising operating pressure: if the system needs progressively more pressure to hold output, membrane resistance is increasing.
- Worsening permeate quality: higher TDS, conductivity or specific contaminants in the permeate indicate lost salt rejection.
- Increasing energy use: higher pump energy to compensate for reduced performance.
- Shortening cleaning intervals: cleaning needed more often than the commissioning baseline means the membrane is likely nearing end of life.
Spotting these early lets you schedule replacement and avoid unplanned downtime and production loss.
Related article: Signs Your RO Membrane Needs Replacement
RO Membrane Cleaning and Maintenance
Routine maintenance is the most reliable way to preserve performance and maximise life. A well-maintained membrane in suitable conditions will outperform a neglected one regardless of its initial quality.
Continuous performance monitoring. Track permeate flow, operating pressure, differential pressure and permeate quality continuously. Normalising data against commissioning baselines separates real performance change from the effect of temperature and flow variation.
Scheduled chemical cleaning (CIP). Clean-in-place uses chemical solutions to remove foulants without removing the membrane from the system. Choose the cleaner by fouling type:
- Alkaline (high pH) cleaners for organic fouling and biofouling
- Acid (low pH) cleaners for scaling and mineral deposits
Schedule cleaning proactively from normalised performance trends, not only after performance has badly deteriorated.
Antiscalant dosing. Antiscalants are chemical inhibitors dosed upstream of the membrane to prevent mineral scale. The right product and dose are critical for hard or high-TDS water. Under-dosing leads to scaling, and over-dosing can cause organic fouling in some systems.
Chlorine management. For TFC membranes, chlorine must be completely removed before the feed reaches the membrane, using activated carbon or sodium metabisulphite. Even brief, low-level exposure causes irreversible oxidation of the polyamide layer.
Pretreatment servicing. Inspect and service sediment filters, carbon filters, softeners, disinfection units and dosing systems regularly. A failure in any of them can quickly become membrane fouling or damage.
Related article: RO Membrane Cleaning vs. Replacement: How to Decide
How to Extend RO Membrane Life
With the right practices, most industrial RO membranes perform reliably for 3 to 5 years. In well-managed systems with good feed water, longer service lives are achievable.
- Invest in effective pretreatment. It affects membrane life more than almost any other factor.
- Monitor performance consistently. Use normalised data to catch fouling trends before they cause damage or lost production.
- Follow a proactive maintenance schedule. Scheduled CIP based on operating hours or performance triggers beats reactive cleaning.
- Manage recovery carefully. Stay within the recommended range for your feed chemistry. Excess recovery accelerates scaling and raises cost.
- Use compatible, approved chemicals. Antiscalants and cleaners must suit your membrane type and be approved by the manufacturer.
- Follow manufacturer operating guidelines. Staying within pressure, temperature and pH limits prevents avoidable degradation.
Popular RO Membrane Brands
Several manufacturers have a strong reputation for consistent quality in industrial water treatment. The brands most widely used in the UAE, GCC and global markets include:
- FilmTec (DuPont): one of the most recognised membrane brands, with a full range for brackish water, seawater and specialty use. Browse FilmTec RO membranes.
- Hydranautics (Nitto): well regarded for high-performance seawater and low-energy membranes. Browse Hydranautics RO membranes.
- LG Chem: known for high-productivity membranes with a good balance of performance and value. Browse LG RO membranes.
- Toray: an established manufacturer with a strong presence in desalination and large industrial projects.
- Vontron: a practical option for cost-sensitive industrial applications.
The best brand depends on feed conditions, required rejection, system design and budget. For a buyer-focused comparison, read Wholesale RO Membranes in UAE: Filmtec, LG and Hydranautics. Where budget is tight and the duty is not critical, refurbished and used RO membranes are an option, with shorter expected life and no guarantee of original performance.
How to Choose the Right RO Membrane
The wrong membrane means poor performance, higher operating cost and shorter life. Use these criteria for every industrial selection.
Feed water analysis. Test TDS, hardness, pH, turbidity, organics, iron, silica and biological activity. This data underpins every other decision and must come before any specification is finalised.
Required permeate quality. Define targets as TDS limits, specific ion rejection or the regulatory standard for your industry, then choose a specification that meets them under expected operating conditions.
Operating pressure and energy. Match the membrane’s pressure needs to your pump capacity and energy budget. BW membranes run at far lower pressure than SW membranes, which directly affects energy cost.
Recovery rate targets. Higher recovery reduces feed and waste volumes, but it must be balanced against feed chemistry to avoid scaling. Set it at design stage, not arbitrarily after installation.
System capacity. Choose element size and quantity to meet permeate output within the system’s hydraulic and pressure limits.
Regulatory and application requirements. Pharmaceutical water, food-grade process water and some municipal uses require specific standards or certifications. Confirm them before you finalise the selection.
The right specification translates directly into better performance, lower total cost of ownership and longer service life.
Why Choose Aqua Flair for RO Membranes in the UAE and GCC?
A reliable supply partner matters as much as the membrane itself. Aqua Flair Trading LLC supplies RO membranes and water treatment equipment across the UAE and GCC, supporting businesses that need dependable products, technical knowledge and responsive service.
Local expertise backed by regional experience. We understand the conditions industries face in this region: high ambient temperatures, hard and high-TDS groundwater, and heavy reliance on desalinated water. That knowledge shapes every recommendation.
Products from recognised manufacturers. We supply industrial elements from FilmTec, Hydranautics, LG Chem, Toray and Vontron, so there is a proven option for each type of application.
Sectors we support.
- Manufacturing: process water and boiler feed water treatment
- Food and beverage: ingredient water and process water systems
- Hotels and hospitality: building water treatment for large commercial properties
- Healthcare: purified water for hospitals, clinics and laboratories
- Commercial and municipal: large-scale water purification systems
Supply beyond the UAE. We also supply customers in Saudi Arabia, Kuwait, Qatar, Oman, Bahrain, Kenya, Rwanda and Angola. You can browse everything we stock on our products page.
Frequently Asked Questions
How long do industrial RO membranes typically last?
Most last between 3 and 5 years under normal conditions. Systems with effective pretreatment and consistent maintenance often last longer. Poor feed quality or inadequate maintenance shortens life.
Can RO membranes be cleaned rather than replaced?
Yes. Chemical cleaning (CIP) can restore performance when fouling is the main cause of decline. If the membrane has suffered physical damage or irreversible chemical degradation, such as chlorine oxidation of a TFC membrane, cleaning will not restore performance and replacement is necessary.
What causes RO membrane fouling?
The four main types are scaling (mineral deposits), biofouling (bacterial biofilm), organic fouling (natural organic matter) and colloidal fouling (fine particles). Each needs its own prevention strategy and cleaning approach.
How often should RO membranes be replaced?
There is no fixed interval. Timing depends on feed quality, operating conditions, maintenance history and actual performance. Normalised permeate flow and salt rejection trends are the most reliable indicators.
What is the difference between BW and SW membranes?
BW membranes are designed for low to moderate salinity and run at lower pressure. SW membranes are built for ocean water and other high-salinity sources, need much higher pressure and deliver higher salt rejection.
Are TFC membranes better than cellulose acetate membranes?
For most industrial applications, yes. TFC offers higher rejection, better flow and longer life. Its key limitation is chlorine sensitivity, so feed must be dechlorinated. CA tolerates limited chlorine but is considered legacy technology in most modern designs.
Can RO membranes remove bacteria and viruses?
Yes, because of their extremely small pore size. RO should not be the sole barrier against biological contamination, though. Pretreatment and disinfection remain important parts of a complete system.
What is the difference between 4040 and 8040 RO membranes?
4040 membranes (4 in × 40 in) suit smaller commercial systems and point-of-use applications. 8040 membranes (8 in × 40 in) are the standard for large industrial plants and deliver much higher permeate flow.
Conclusion
RO membranes are the most critical performance component in an industrial water treatment system. Their ability to remove dissolved salts, contaminants and microorganisms makes them indispensable in sectors from food production and pharmaceuticals to desalination and manufacturing.
Getting the most from them is not only about choosing the right product. Effective pretreatment, sound system design, ongoing monitoring and a consistent maintenance programme work together to give reliable output, longer membrane life and lower operating cost. The related articles linked throughout this guide go deeper on fouling types, cleaning protocols, brand comparisons and replacement decisions.
For businesses in the UAE and GCC, Aqua Flair Trading LLC can help with the right products, regional expertise and technical guidance. Request a quote with your feed water analysis and system details, and our team will recommend a suitable configuration.
Share this story


